In 2026, manufacturers face a practical question: how to improve the impact resistance of PS sheets without sacrificing clarity, stiffness, or production efficiency? Polystyrene remains valuable for displays, packaging, insulation, and protective components. PlasticsEurope’s Plastics—The Facts 2023 reports that global plastics production reached 400.3 million tonnes in 2022. That scale increases pressure to make every sheet last longer.
Impact performance begins with material selection. General-purpose polystyrene is rigid, but it can fracture under sudden loading. High-impact polystyrene, or HIPS, adds rubber-based modification for greater toughness. The trade-off is real. Higher rubber content may reduce transparency, surface hardness, or dimensional stability. Processing also matters. Poor drying, uneven cooling, sharp corners, and excessive residual stress can create weak zones around drilled holes or formed edges.
Test before changing everything.
ASTM D256 and ISO 179 provide recognized methods for measuring notched impact strength. However, laboratory results may not represent a dropped tray, a cold warehouse panel, or repeated handling on a production line. Real-use testing should include temperature cycling, edge impacts, thickness variation, and aging. The OECD’s Global Plastics Outlook highlights growing pressure to improve plastic resource efficiency and product durability. Longer service life supports that direction, but durability claims still need evidence.
A stronger PS sheet may require rubber modification, optimized extrusion temperature, slower cooling, or redesigned geometry. No single adjustment works universally. This guide examines how to improve the impact resistance of PS sheets through formulation, processing control, structural design, and validation. Some recommendations may need further testing. That uncertainty is important. Reliable engineering begins there.
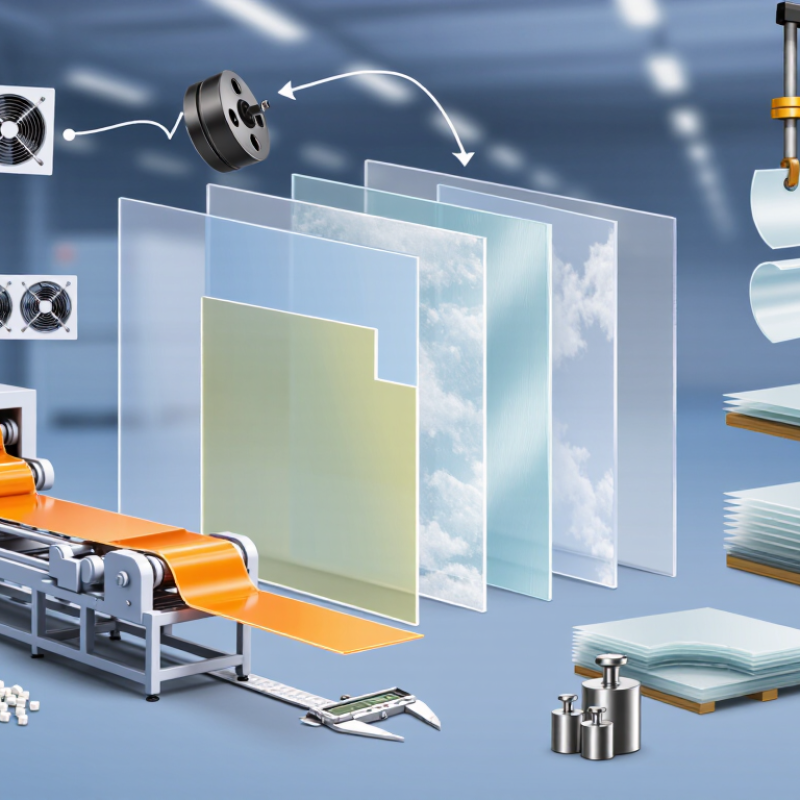
How to Improve the Impact Resistance of PS Sheets in 2026?
ASTM D256 highlights a significant performance gap between common polystyrene grades. Public technical data compilations typically place GPPS near 10–20 J/m, while HIPS often reaches 60–150 J/m. These values are useful benchmarks, not universal guarantees. Specimen thickness, notch quality, temperature, and conditioning can change the result considerably.
The gap is real. GPPS is rigid and visually clear, but its brittle fracture can appear suddenly around drilled holes or sharp corners. HIPS uses a dispersed rubber phase to absorb more impact energy. The PlasticsEurope Plastics—The Facts 2024 report confirms the continuing industrial importance of styrenic plastics, while ASTM D256 remains a practical reference for comparing notched impact performance.
Manufacturers improving PS sheets should start with controlled formulation trials. Increasing rubber modification may raise toughness, but excessive rubber can reduce clarity, stiffness, or surface quality. Sheet extrusion also matters: uneven cooling can create internal stress, making laboratory results look better than field performance. Test samples should match the final thickness and processing history.
A useful 2026 target is not simply “maximum impact.” It is repeatable performance near the intended application range. Record notch geometry, conditioning temperature, failure mode, and batch variation. One overlooked detail can distort the comparison. More testing is still needed for thin sheets exposed to cold outdoor service, where HIPS may lose part of its impact advantage.
GPPS commonly measures about 10–20 J/m under standard conditions. HIPS often reaches 60–150 J/m. These are benchmarks, not guarantees. Thickness, temperature, and notch quality can change results.
GPPS is rigid and clear, but it can fracture suddenly. Drilled holes and sharp corners concentrate stress. Rounded edges may reduce cracking. The improvement is not always consistent.
Keep the melt profile near 200–240°C. Adjust temperature gradually. Excessive heat may reduce molecular weight. Low heat can leave unmelted particles and brittle points. Watch melt behavior, not only barrel readings.
It is extremely important. A practical target is often within ±3% of the specified gauge. Even a 0.2-millimeter difference can change drop-test failures. Check thickness across the entire sheet width.
Yes, dispersed rubber can absorb more impact energy. However, excessive rubber may reduce clarity, stiffness, or surface quality. Tougher is not automatically better. The correct balance depends on the application.
Use ASTM D256 or ISO 179 with matched specimens. Record thickness, notch geometry, conditioning time, and test temperature. Test both notched and unnotched samples. Test twice. Keep failed samples in the records.
A practical target is at least 20% above the untreated control. Use the same batch and cutting method. Repeat the measurements. A single strong result proves very little.
Condition finished sheets at the expected low temperature. Then perform controlled drop testing and inspect the impact area. Look for whitening, splits, and delayed cracks. HIPS may lose some advantage in cold conditions. More testing is needed.
Uneven cooling can create internal stress. Short residence time and steady haul-off speed usually help. Record failure modes and batch variation. I would not trust laboratory data without matching processing history.
To understand how to improve the impact resistance of PS sheets in 2026, begin by establishing a reliable performance benchmark. General-purpose polystyrene (GPPS) typically delivers around 10–20 J/m, while high-impact polystyrene (HIPS) can reach approximately 60–150 J/m when tested under ASTM D256. Adding 5–15 wt% of a suitable rubber modifier can significantly improve toughness while helping control haze and maintain acceptable appearance.
Processing conditions are equally important. Extrusion should generally be optimized within 200–240°C, with careful control of melt flow and sheet thickness to prevent weak areas. Post-extrusion annealing at 80–100°C can reduce residual stress, lowering the risk of cracking during handling or use. Finally, validate the finished sheets using ASTM D256 or ISO 179 and compare the results with the original baseline. A practical development target is at least a 20% improvement in impact strength without sacrificing dimensional stability or surface quality.
 Benchmark Plastic